
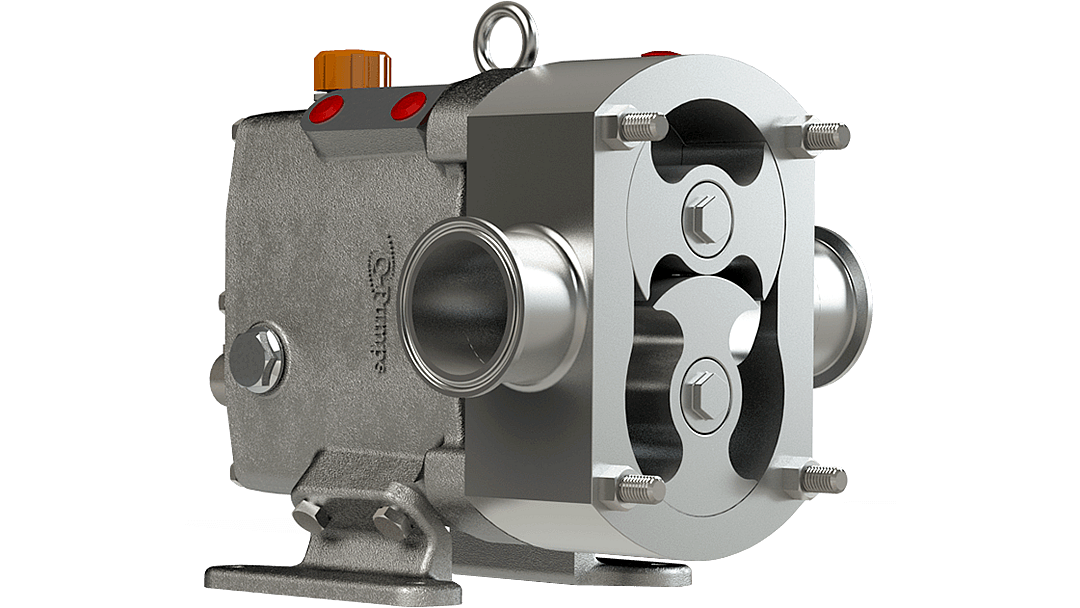
Rotary Lobe Pump QL Series
Economical High Performance Rotary Lobe Pump
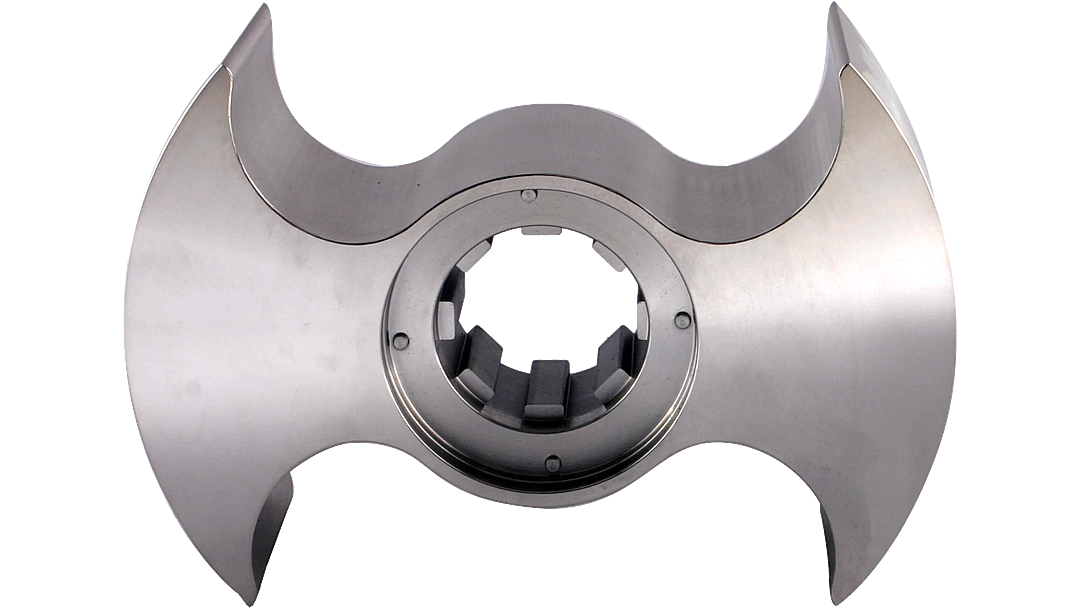
Bi-wing Rotor
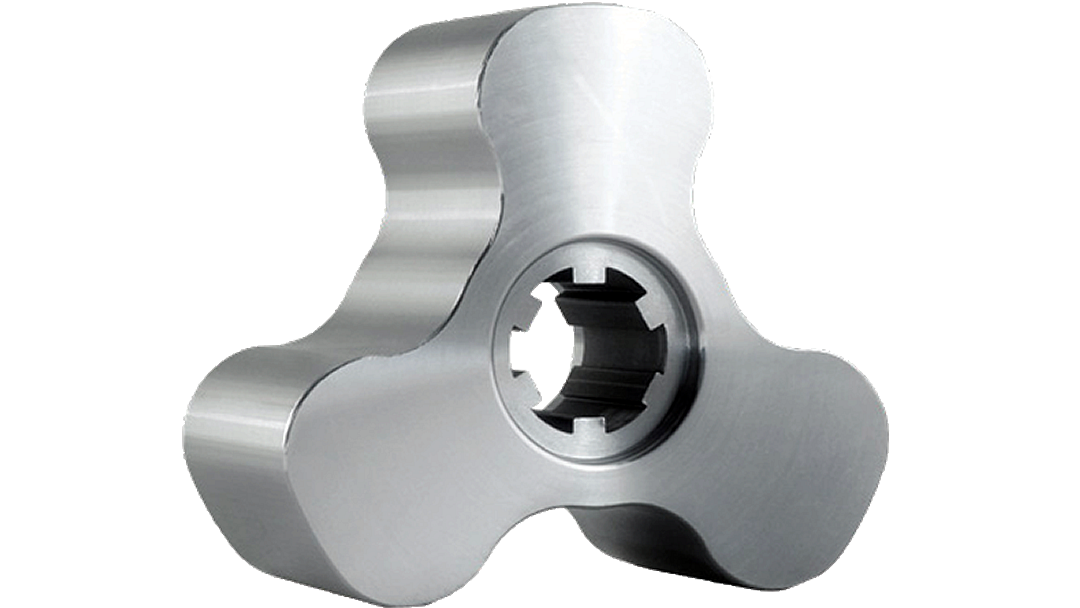
Tri-lobe Rotor
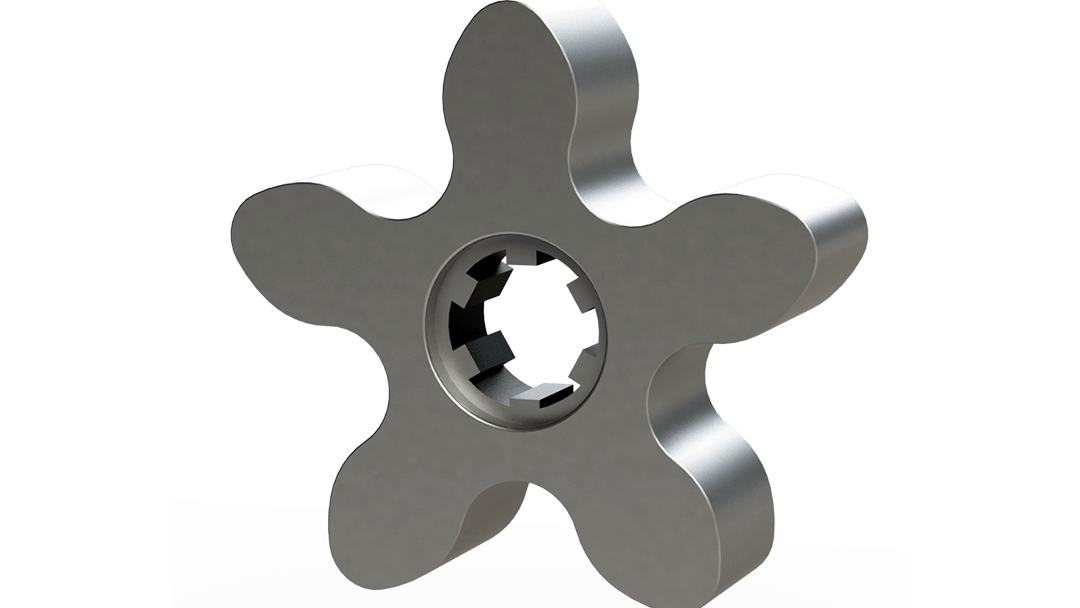
Multi-lobe Rotor
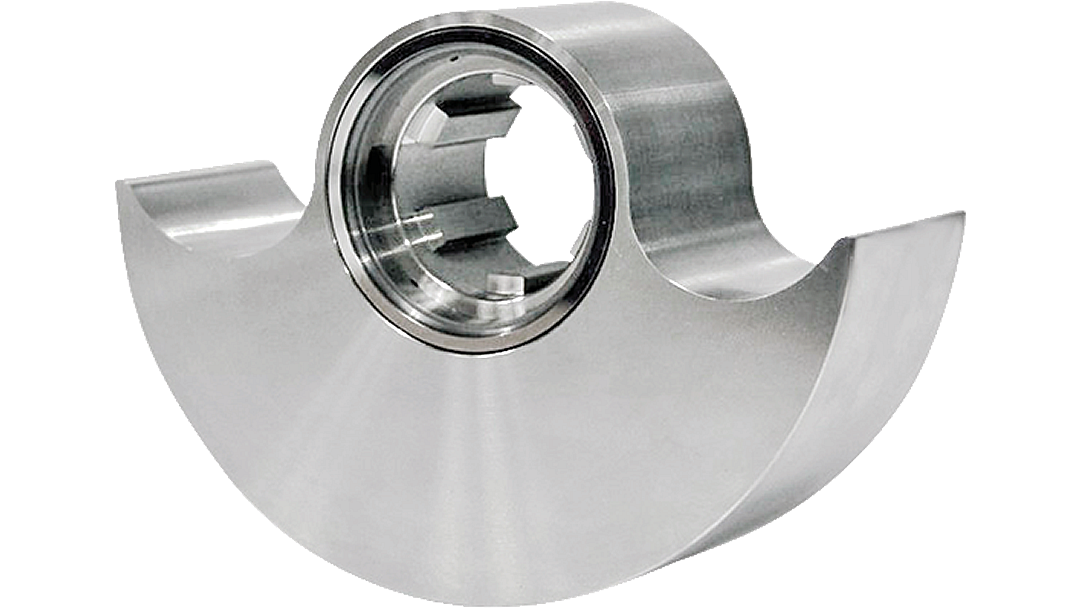
Single Wing Rotor
QL Series Lobe Pump Performance
Capacity
0 to 100m³ per hour
Pressure
0 to 20 bar
Viscosity
Up to 1,000,000 centiPoise
Temperature
To 150°C
QL Series Lobe Pump Characteristics
Ease of maintenance, economic price and ‘clean-in-place’ CIP performance are key features of the QL positive displacement rotary lobe pump.
Its front loading seal is ideal for easy and fast maintenance as there is no need to remove piping to gain access to the seals – simply remove the front cover and rotors.
Rotor Options
Different rotor options to meet your product handling requirements.
- Bi-Wing Rotor (standard)
- Tri-Lobe Rotor
- Multi-Lobe Rotor
- Single-Wing Rotor
Hygienic Standards Compliant
- 3-A certified and designed to comply with EHEDG standards
- Wetted parts in 316 Stainless Steel 316L
- Bearing housing in 304 stainless-steel (no paint)
Port Options
Tri-clamp connections as standard with other sanitary and industrial ports available
Surface Finish
- 32 µin (.8 µm) Ra maximum surface finish
- Optional electropolished finish in wetted parts
Sealing Options
Standard mechanical seal faces in Tungsten Carbide with many options and materials to choose from including:
- Single O-ring Seal
- Single Mechanical Seal
- Double Mechanical Seal
- Triple Lip Seal
Features & Benefits
High performance lobe pump
- Four different sealing types to cover every application
- Front cover and pump casing water jacket options for heating / cooling in temperature sensitive applications
- Toughened surface options available for handling abrasive products
Easy maintenance lobe pump
- Front access for quick cleaning and less downtime
QL Series Rotary Lobe Pump Models & Specifications
| Lobe Pump Model | Port Size | Flow m³/hr | Max RPM | Max Pressure BAR |
| QL-A10 | 1-inch / DN25 | 3 | 1000 | 20 |
| QL-A15 | 1.5-inch / DN40 | 5.8 | 800 | 12 |
| QL-A20 | 2-inch / DN50 | 10 | 800 | 8 |
| QL-B20 | 2-inch / DN50 | 17.2 | 700 | 12 |
| QL-B25 | 2.5-inch / DN65 | 26 | 700 | 8 |
| QL-C30 | 3-inch / DN80 | 36.7 | 600 | 12 |
| QL-C40 | 4-inch / DN100 | 51.8 | 600 | 8 |
Lobe Pump Spare Parts
Source genuine spare parts and convenient pump repair / service kits from BestPump – Q-Pumps authorised UK distributor.
Call us now on +44 (0) 1236 433 799.
Lobe Pump Repairs
Entrust your lobe pump repairs to BestPump’s manufacturer-approved engineers and workshop for service and repairs for all pump types and brands.
Call us now on +44 (0) 1236 433 799.
Why choose the QL Rotary Lobe Pump?
The ubiquitous lobe pump has been producing Britain’s food, beverage, cosmetics and pharmaceuticals for many years.
9 Features of the QL Lobe Pump (and how they help you)
- Hygienic Design:
The pump has an hygienic design to ensure the safe handling of food products and compliance with food safety regulations. Standard features include smooth surfaces, sanitary seals, and easy disassembly for thorough cleaning and sanitation. - Material Compatibility:
The pump materials offer compatibility with the specific food products you handle in your facility. Stainless steel construction for its corrosion resistance and durability, especially when dealing with acidic or corrosive food ingredients. - Gentle Product Handling:
The QL lobe pump is capable of gently handling delicate food products without causing damage or degradation. This is particularly important for products such as dairy, sauces, and purees where maintaining product integrity is critical. - Efficiency and Performance:
Proven high efficiency and excellent performance metrics, including flow rate, pressure capabilities, and energy efficiency. These lobe pumps are able to meet your production requirements while minimising downtime and energy consumption. - Ease of Maintenance:
The pumps are easy to maintain to minimise downtime and ensure optimal performance. Features such as simple disassembly, quick access to internal components, and readily available spare parts repair kits from stock held in the UK. - Reliability and Durability:
Reliability is paramount in food production to ensure consistent output and prevent disruptions to our operations. These lobe pumps have a proven track record of reliability and durability in food processing and hygienic applications. - Compliance with Standards:
The pump comply with relevant industry standards and regulations, such as 3-A Sanitary Standards to provide you with assurance of product safety and quality. - Support and Service:
BestPump is directly backed by the manufacturer and we strive to maintain our reputation for customer support, technical assistance and after-sales service. Prompt support and assistance are crucial for addressing any issues that may arise during operation and ensuring smooth production – trust BestPump to deliver! - Cost-effectiveness:
While upfront cost is important, you will also consider the total cost of ownership over the pump’s lifespan, including maintenance, energy consumption, and downtime costs. The QL lobe pump offers long-term reliability and efficiency to provide best value in the long run.
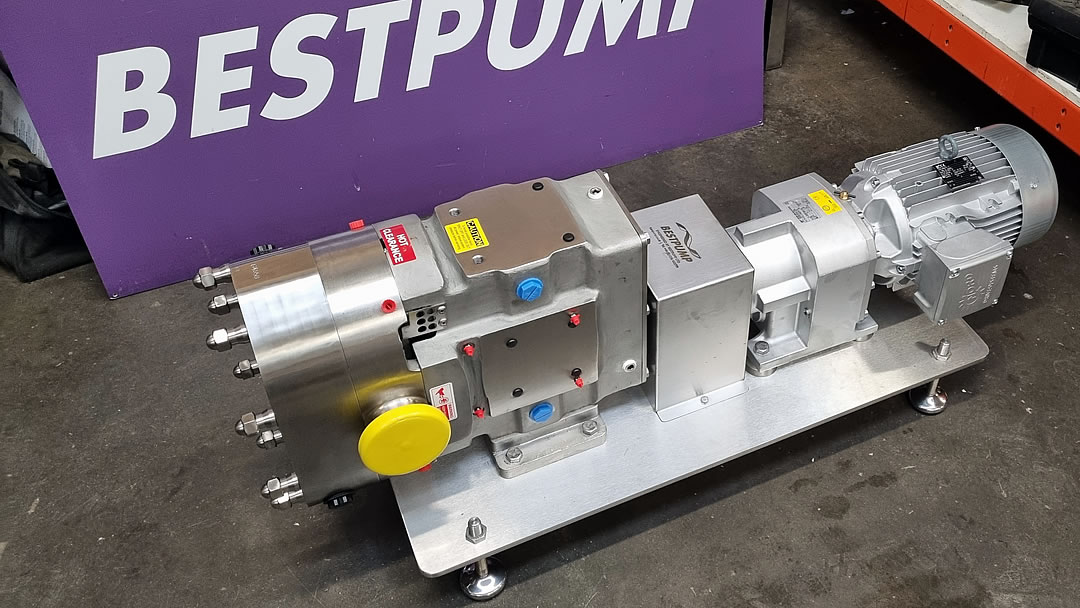
Pump Skids
When you need your pumps motorised and skid mounted, our design and fabrication capabilities are at your disposal.
From pump selection to mounting, BestPump will work with you to produce bespoke pump skids to your specifications and dimensions.